 Contact Us
 Home /
What Is CNC Milling and How Does the Process Work?


Table of Contents
- From CAD Design to a Machined Part
- Workpiece Preparation and Setup
- Common CNC Milling Operations
- Roughing and Finishing
- Cutting Tools Used in CNC Milling
- Understanding CNC Milling Axes
- Materials Suitable for CNC Milling
- Factors That Affect Milling Accuracy
- Surface Finish in CNC Milling
- CNC Milling Inspection
- Typical CNC-Milled Components
- Why CNC Milling Is Widely Used

CNC milling is a computer-controlled subtractive manufacturing process used to create precise components from solid material. During machining, a rotating cutting tool removes material from a workpiece according to programmed toolpaths.
The process can produce flat surfaces, pockets, slots, holes, threads, contours, angled features, and complex three-dimensional geometries. CNC milling is commonly used for prototypes, fixtures, molds, housings, brackets, manifolds, and production components across industrial, automotive, medical, electronics, and aerospace applications.
Unlike CNC turning, where the workpiece rotates, CNC milling normally keeps the workpiece fixed while the cutting tool rotates and moves along one or more controlled axes.
From CAD Design to a Machined Part
Every CNC milling project begins with a digital design. Engineers usually provide a 3D CAD model together with a 2D technical drawing.
The 3D model defines the component geometry, while the drawing communicates manufacturing requirements that may not be fully represented in the model, including:
- Dimensional tolerances
- Geometric tolerances
- Surface roughness
- Thread specifications
- Material grade
- Datum references
- Heat treatment
- Surface finishing
- Inspection requirements
The CAD model is imported into CAM software, where a programmer develops the machining strategy.
CAM programming determines:
- Tool selection
- Cutting sequence
- Spindle speed
- Feed rate
- Depth of cut
- Tool engagement
- Entry and exit movements
- Roughing and finishing paths
- Workpiece orientation
The toolpaths are then converted into machine-readable instructions, commonly called G-code.
Before production, the program may be simulated to identify potential collisions, excessive tool movement, poor feature access, or inefficient cutting paths.
Workpiece Preparation and Setup
The selected raw material may be supplied as a plate, block, bar, casting, or near-net-shape blank. It is cut to an appropriate size before being installed in the milling machine.
The workpiece must be held securely using suitable workholding equipment, such as:
- Machine vises
- Clamps
- Fixture plates
- Soft jaws
- Vacuum fixtures
- Modular fixtures
- Custom workholding systems
Workholding must resist cutting forces without deforming or damaging the part.
The setup also determines which surfaces can be machined during one operation. If the cutting tool cannot reach all required features, the component may need to be repositioned or transferred to another fixture.
Repeated repositioning increases setup time and may introduce alignment variation between features. For this reason, process engineers often try to machine as many critical surfaces as possible from a common setup.
Common CNC Milling Operations
CNC milling machines can perform many operations using different cutting tools.
Face Milling
Face milling creates broad, flat surfaces. It is often used to establish a reference surface or reduce the raw material to the required thickness.
Pocket Milling
Pocket milling removes material from an enclosed area. Pockets may be shallow, deep, rectangular, circular, or irregularly shaped.
Profile Milling
Profile milling follows the external or internal contour of a component. It is commonly used to create final outer shapes and curved boundaries.
Slot Milling
Slot milling produces grooves, channels, keyways, and narrow internal features.
Drilling
Drilling creates round holes using rotating drill tools. Additional operations may be required when a hole needs higher accuracy or a smoother internal surface.
Reaming and Boring
Reaming and boring improve the diameter, roundness, position, or surface quality of an existing hole.
Tapping and Thread Milling
Internal threads can be produced by tapping or thread milling. Thread milling can be useful for larger diameters, difficult materials, or applications requiring greater process control.
Chamfering
Chamfer tools remove sharp edges and create angled transitions around holes and external profiles.
Three-Dimensional Contouring
Ball-nose and specialty end mills can machine molds, curved housings, impellers, and other free-form surfaces.
Roughing and Finishing
Most CNC milling operations include separate roughing and finishing stages.
Roughing removes large amounts of material as efficiently as possible. The objective is to create the approximate shape while leaving a controlled amount of material for finishing.
Modern roughing strategies may use constant tool engagement or adaptive toolpaths to reduce sudden changes in cutting load.
Finishing uses lighter cuts to achieve final dimensions, surface quality, and geometric accuracy. Finishing tools may follow the same area several times using different orientations or step-over distances.
Separating roughing and finishing is important because heavy material removal can generate:
- Cutting heat
- Internal stress
- Tool deflection
- Workpiece deformation
- Surface vibration
Allowing the part to stabilize before final finishing can improve dimensional consistency.
Cutting Tools Used in CNC Milling
The correct cutting tool depends on the material, geometry, depth, and required finish.
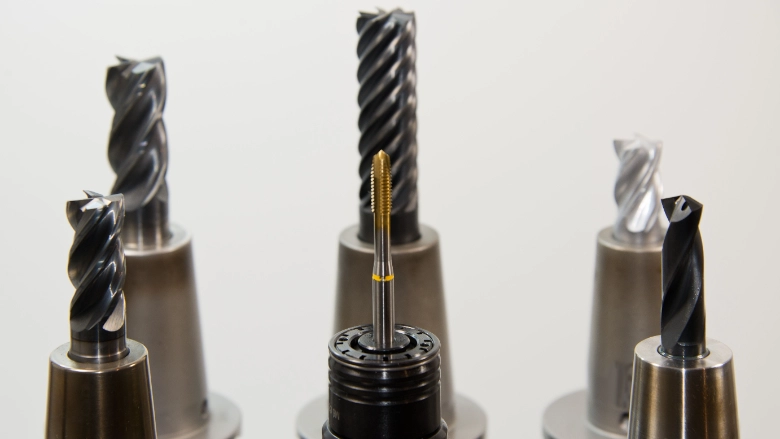
Common milling tools include:
- Flat end mills
- Ball-nose end mills
- Corner-radius end mills
- Face mills
- Drills
- Reamers
- Thread mills
- Chamfer mills
- T-slot cutters
- Dovetail cutters
- Boring tools
Tool diameter influences the smallest internal corner that can be machined. Tool length influences the maximum accessible depth.
Long tools can reach deep cavities, but they are less rigid and more likely to deflect or vibrate. Designers should therefore avoid unnecessarily deep, narrow features.
Understanding CNC Milling Axes
A standard 3-axis milling machine moves along the X, Y, and Z directions.
These axes allow the tool to move:
- Left and right
- Forward and backward
- Up and down
Three-axis milling is suitable for many plates, brackets, housings, and fixtures.
Four-axis machines add a rotary axis, allowing the workpiece to rotate during or between machining operations. This can make it easier to machine features around cylindrical or multi-sided components.
Five-axis machines add two rotary movements. They can position or continuously move the workpiece relative to the cutting tool, improving access to complex surfaces and angled features
Materials Suitable for CNC Milling
CNC milling supports a wide range of metals and engineering plastics.
Common metals include:
- Aluminum
- Stainless steel
- Carbon steel
- Alloy steel
- Brass
- Copper
- Titanium
Common plastics include:
- POM
- PEEK
- Nylon
- Polycarbonate
- PTFE
- ABS
Every material requires an appropriate cutting strategy.
Aluminum generally allows high cutting speeds and efficient material removal. Stainless steel requires careful control of heat, tool wear, and work hardening.
Titanium has a high strength-to-weight ratio but can retain heat near the cutting edge. Copper may produce burrs or adhesive tool wear because of its ductility.
Engineering plastics may expand under heat or deform under clamping pressure. Moisture absorption can also influence the dimensions of some materials.
Factors That Affect Milling Accuracy
CNC milling accuracy depends on the entire manufacturing system rather than the machine alone.
Important factors include:
- Machine condition and calibration
- Tool rigidity
- Tool wear
- Workpiece stability
- Fixture accuracy
- Material stress
- Cutting temperature
- Part geometry
- Wall thickness
- Feature depth
- Programming strategy
- Inspection method
For example, a thick aluminum block with accessible features may be easier to control than a large, thin plastic panel, even when both drawings specify the same tolerance.
Surface Finish in CNC Milling
Surface roughness is influenced by tool condition, tool geometry, spindle speed, feed rate, step-over, vibration, and material properties.
A smooth machined surface may require:
- A dedicated finishing tool
- Reduced feed per tooth
- Smaller step-over distances
- Stable workholding
- Additional finishing passes
- Controlled tool engagement
Post-machining processes such as sanding, polishing, bead blasting, anodizing, plating, painting, or powder coating may also be used.
Surface finishing should be considered during design because some treatments add thickness or alter the original machined surface.
CNC Milling Inspection
Inspection confirms that the manufactured part meets the drawing requirements.
Common inspection equipment includes:
- Vernier calipers
- Micrometers
- Height gauges
- Pin gauges
- Thread gauges
- Optical measuring systems
- Surface roughness testers
- Coordinate measuring machines
Simple dimensions may be checked directly at the machine. Complex profiles, positions, and geometric tolerances may require CMM inspection.
Typical CNC-Milled Components
CNC milling is widely used to produce:
- Mechanical housings
- Electronic enclosures
- Mounting brackets
- Heat sinks
- Valve bodies
- Fluid manifolds
- Mold inserts
- Precision fixtures
- Medical equipment components
- Aerospace structural parts
Why CNC Milling Is Widely Used
CNC milling offers a flexible path from digital design to finished component. It does not require dedicated production tooling for every new part, making it suitable for prototypes and low-volume manufacturing.
The same process can also be scaled for repeat production when stable programs, fixtures, tooling, and inspection methods are established.
Successful CNC milling depends on more than machine capability. Appropriate material selection, practical tolerances, accessible geometry, stable workholding, and clear drawings all contribute to reliable production.
When product designers and machining engineers consider these factors early, CNC milling can deliver an effective balance of accuracy, flexibility, lead time, and cost.
Talk to the Manufacturer, Not a Middleman
Resources & Insights
-
 Engineering Resource Hub
How Custom Manufacturing Orders Work: A Step-by-Step Guide
2026-08-05By Karry Precision -
 Engineering Resource Hub
Why CNC Milling Remains Essential for High-Performance Industries
2026-08-05By Karry Precision -
 Engineering Resource Hub
How to Evaluate a CNC Milling Supplier Beyond the Quoted Price
2026-08-05By Karry Precision -
 Engineering Resource Hub
From Prototype to Production: How CNC Milling Supports Product Development
2026-08-05By Karry Precision